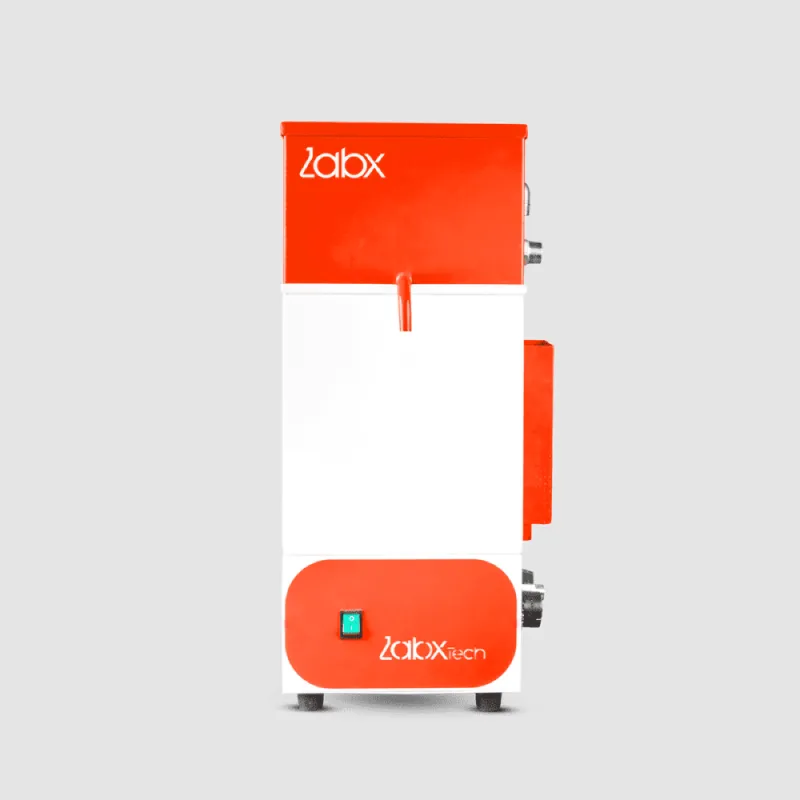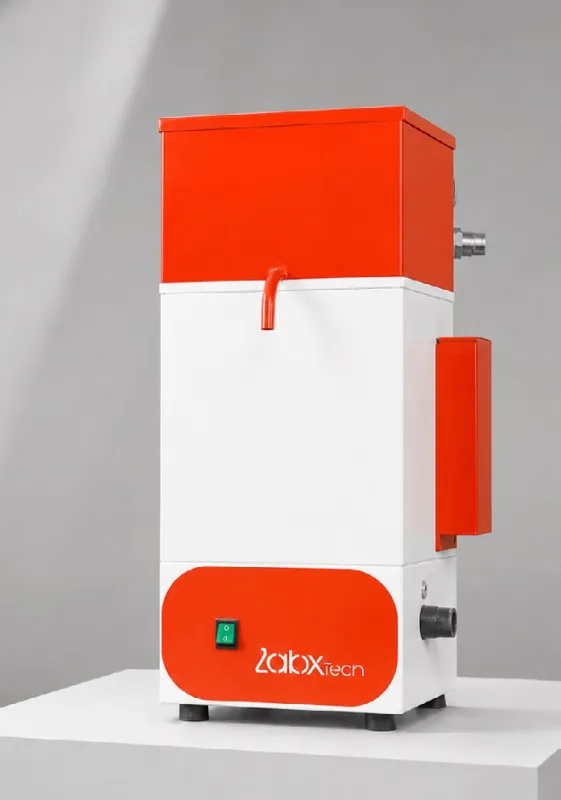
Double Water Distillation Unit
Two-stage stainless steel distiller with an internal storage tank for ultra-pure water.
Overview
The LabX Double Water Distillation Unit is engineered to produce ultra-pure distilled water using a two-stage distillation process, ensuring significantly higher purity compared to single-stage systems.
It is designed for demanding applications in laboratories, hospitals, pharmaceutical facilities, and industrial environments that require consistent ultra-clean water quality and high operational reliability.
The unit is constructed entirely from high-grade stainless steel, with an electrostatically coated outer body for enhanced protection against humidity, corrosion, and harsh environments. It also includes an internal storage tank to collect and stabilize distilled water before dispensing.
Key features
Dual independent boilers
- Two boilers operating in parallel for higher efficiency and continuous production
- Each boiler has an independent heating and safety system
Internal collection tank
- Integrated tank for storing distilled water before use
- Ensures smooth and consistent water dispensing
- Eliminates the need for external storage containers
Durable external protection
- Electrostatically coated outer body
- Resistant to rust, moisture, and chemical exposure
- Easy to clean and maintain
Full safety system
- Mechanical water level sensors
- Overheat protection system
- Dry-run protection (automatic shut-off)
- Pressure relief valve for safe operation
Efficient cooling system
- Built-in heat exchanger
- Reduces cooling water consumption
- Improves overall energy efficiency
Manual operation
- Simple mechanical switch control system
- No electronic components for higher reliability
- Reduces maintenance and failure risks
Note
Each boiler is equipped with its own heating element and independent safety system to ensure stable and continuous double-stage operation.
Water output quality
- Conductivity
- Approx. 1.0 µS/cm at 25°C
- pH range
- 6.0 – 7.0 (ideal for sensitive scientific and medical applications)
Technical advantages
- Double-stage distillation ensures ultra-high purity water
- Complete safety system for overheating, dry-run, and overpressure protection
- Robust, electronic-free design for maximum reliability and low maintenance
- Efficient cooling system reduces water and energy consumption
Applications
- Research and analytical laboratories
- Hospitals and medical sterilization systems (autoclaves)
- Pharmaceutical production
- Industrial processes requiring ultra-pure water
Why choose LabX?
- Ultra-high purity water output
- Heavy-duty industrial construction for long service life
- Fully manual and highly reliable operation
- Efficient cooling and energy optimization
- Strong after-sales support and spare parts availability
LabX Tech statement
At LabX Tech, we deliver advanced water purification systems designed for maximum purity, operational safety, and long-term industrial reliability, supporting critical scientific and medical applications worldwide.
Original datasheets
Warranty
- One-year comprehensive warranty on all devices
- Two-year warranty against manufacturing defects
- Maintenance contract after the warranty period